If you’ve ever worked with fluid transfer systems, you know that pump castings are the unsung heroes of these operations. As a pump castings supplier with over a decade in this industry, I’ve seen firsthand how a poorly installed casting can turn a smooth-running pump into a maintenance nightmare—think unexpected downtime, higher energy bills, or even full system failures. That’s why I want to walk you through the installation guidelines I’ve honed over years of working with plant engineers, maintenance teams, and system integrators. These aren’t just textbook rules; they’re lessons learned from troubleshooting projects where cut corners led to costly mistakes. Pump Castings

First, before you even touch a wrench, you need to do your pre-installation checks. A lot of people skip this step and end up with avoidable issues down the line. Let’s start with inspecting the pump casting itself. When our castings leave our facility, we mark them with unique serial numbers and quality control stamps—this isn’t just for our records, it’s so you can trace every part back to its production batch. When you receive the casting, start by unpacking it carefully: avoid dropping it or letting it bang against other equipment, even if it feels heavy and durable. I once worked with a plant team that rushed unpacking and nicked the impeller eye of a cast iron centrifugal pump casing; by the time they installed it, the nick had caused cavitation that rattled the entire system within three months. So run your hands (wear clean cotton gloves, by the way—oil or dirt from skin can corrode the casting surface over time) along all internal and external surfaces, looking for any scratches, porosity, or misaligned machined faces. If you find anything, contact your supplier immediately—we replaced that damaged casting for the team that day, no questions asked, which saved them from a full shutdown.
Next, verify that the casting matches your order specifications. This might sound basic, but you’d be surprised how often mix-ups happen. Check the material grade (whether it’s ductile iron, bronze, stainless steel, or one of the custom alloys we offer), the discharge and suction flange sizes, the bolt hole patterns, and the impeller clearance dimensions. If you’re using a custom casting for a specific application—like a high-pressure pump for oil and gas, or a corrosion-resistant one for chemical processing—double-check the dimensional prints we provided. I’ve had a customer tell me a casting “didn’t fit” only to realize they’d ordered a 6×4 inch casing but pulled a 5×3 from stock. Taking 10 minutes to confirm specs now can save hours of rework later. Also, check for any protective coatings we applied for shipping—most of our pump castings have a light rust-inhibiting film, so you’ll need to remove this with a mild, non-abrasive solvent before installation; don’t use a wire brush here, as it can scratch the machined sealing surfaces.
Once you’ve confirmed the casting is intact and correct, move on to preparing the pump base and adjacent components. The base is the foundation for the entire pump assembly, and a level, rigid base is non-negotiable. If the base is made of concrete, make sure it’s fully cured (wait at least 28 days for new concrete, as we learned the hard way when a team installed a pump on a 10-day-old base that shifted under load). If it’s a steel base, check for any warping or rust that might create uneven support. Use a precision level (a 2-foot machinist’s level is best, not a small torpedo level) to check the base along both the length and width. Shims will be your best friend here—use only mild steel shims, not plastic or wood, as they can compress over time. Place shims in pairs near each mounting bolt, and don’t use more than three shims per bolt; if you need more, trim the base or add a reinforcing plate. Tighten the mounting bolts slightly, then recheck the level—you’d be surprised how even a 0.005 inch per foot tilt can cause misalignment between the pump casting and the driver (motor or engine).
Speaking of alignment, this is one of the most critical steps for pump casting installation, and it’s where most errors occur. There are two types of alignment: angular alignment (where the shafts of the pump and driver are at an angle to each other) and parallel alignment (where the shafts are offset side to side). Misalignment, even minor, puts excessive stress on the pump casing’s shaft seals, bearings, and impeller, leading to premature wear. When aligning, use a dial indicator for accuracy—eyeballing it with a straight edge won’t cut it. The target alignment is usually within 0.002 inches of parallel and 0.001 inches of angular offset for most standard pumps, though we provide specific alignment tolerances for each casting model in our installation guides. If you’re working with a vertical pump casting, the alignment process is a bit different, but the core rule remains: no stress between the pump and driver shafts. I once had a chemical plant client that experienced a seal failure every 3 months on a vertical pump; after we checked alignment, we found the angular offset was 0.01 inches—well over the tolerance. Adjusting the base shims fixed the issue, and their seal life jumped to 18 months.
Next up is installing the pump casting’s internal components, starting with the impeller. First, verify the impeller matches the casing: for most centrifugal pump castings, the impeller is specifically machined to fit the casing’s volute or diffuser. Lubricate the impeller hub with a small amount of food-grade grease (if your application requires it) to make sliding it onto the shaft easier, but don’t over-lubricate—excess grease can get into the volute and cause flow issues later. Tighten the impeller nut to the manufacturer’s specified torque; over-tightening can crack the impeller or the casting’s internal hub, while under-tightening can cause the impeller to slip. Use a torque wrench, and follow the values we provide—they’re calculated based on the casting’s material and the operating pressure it’s designed for.
Then comes the shaft seal, a part that relies heavily on the casting’s sealing surfaces. Whether you’re using a mechanical seal or a packing gland, make sure the seal faces are clean and free of nicks. For the mechanical seal, apply a thin layer of compatible sealant (as recommended for your fluid and material grade) to the gland flange to prevent leaks. When securing the seal to the casting, don’t overtighten the gland bolts—alternate tightening each bolt a quarter turn at a time to ensure even pressure; uneven pressure can cause the seal to bind or leak. If you’re using packing, adjust the gland bolts so you can still turn the packing by hand, then tighten them another quarter turn; if you tighten it too much, the packing will overheat and wear out quickly.
Once the internal components are in place, you’ll connect the suction and discharge piping to the pump casting. This is where many installers make the mistake of forcing piping into alignment with the pump, which creates stress on the casting’s flanges. The rule here is: pipe alignment comes first, then connect to the pump. If the piping is misaligned, the stress will transfer to the pump casing, leading to flange cracking or shaft misalignment over time. Use expansion joints or flexible connectors if your piping system has thermal expansion or vibration—especially for high-temperature or high-pressure applications. Also, make sure to support the suction and discharge piping independently, not relying on the pump to hold their weight. We’ve seen pump castings with cracked flanges just because a 10-foot discharge pipe was left unsupported, pulling on the casing every time the pump ran.
Before you start the pump, do a final pre-start check. First, check all bolt connections: mounting bolts, flange bolts, impeller nut, seal gland bolts. Run a finger along all flanges to make sure there are no gaps—even a small gap here can cause leaks. For suction side, ensure there’s no air entrainment: if you’re pumping liquid, prime the pump completely before starting it, and check that the suction line is fully filled. Air in the suction line causes cavitation, which can erode the pump casting’s internal surfaces over time. I remember a water treatment plant that didn’t prime their pump fully, and within six months, the volute of the cast iron casting had deep pits from cavitation—we had to replace the entire casting, which cost them a week of downtime. Also, check the lubrication for the pump bearings, if applicable, and make sure all guards are in place for moving parts.
Once all checks are done, start the pump slowly and run it for 15 to 30 minutes at low speed, monitoring for any unusual noises, leaks, or vibrations. If you hear grinding, squealing, or rattling, turn the pump off immediately—don’t let it run, as this can cause serious damage. Common issues here are misalignment, impeller touching the casing, or insufficient lubrication. After the initial run, shut the pump down, recheck all connections and alignment, and then run it at full operating speed for an hour, monitoring pressure and flow rates to ensure they match the system design.
Now, I know this might seem like a lot of steps, but every one of them is there to protect your pump casting, which is the most critical part of your fluid system. As a pump castings supplier, our job isn’t just to send you a part—it’s to make sure that part works for you, for years to come. If you have questions about a specific casting model, application, or installation issue, don’t hesitate to reach out. There’s no such thing as a “silly question” when it comes to getting your system right.
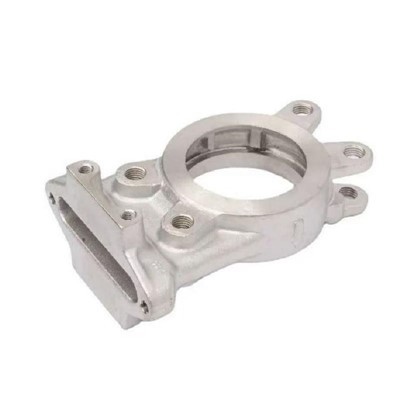
At the end of the day, the success of your pump system starts with a properly installed pump casting. Rushing through installation saves you time in the short term, but leads to costly repairs, downtime, and replacements down the line. Take the time to do it right, and your pump will run efficiently, reliably, for years. If you’re looking for high-quality, precision-machined pump castings tailored to your application, or have questions about installation best practices, we’d be glad to connect. Reach out to our team to discuss your project and find the right solution for your needs.
Stainless Steel Fittings References
- Hydraulic Institute. Pump Installation, Operation, and Maintenance Guidelines. Hydraulic Institute, 2021.
- American Petroleum Institute. API Standard 610: Centrifugal Pumps for Petroleum, Heavy Chemical, and Gas Industry. American Petroleum Institute, 2020.
- The Society of Manufacturing Engineers. Casting Installation and Maintenance for Industrial Fluid Systems. SME Press, 2019.
- Pump Manufacturers Association. Best Practices for Pump Alignment and Component Installation. Pump Manufacturers Association, 2022.
Shandong Shunye Stainless Steel Co., Ltd.
Shandong Shunye Stainless Steel Co., Ltd. is one of the most professional pump castings manufacturers and suppliers in China, also supports customized service. Welcome to buy bulk cheap pump castings made in China here and get quotation from our factory. For price consultation, contact us.
Address: Shandong Province, Binzhou City, Wudi County, Liubao Town, Zhangdong Road, Duliucun Village
E-mail: sales@wdshunye.com
WebSite: https://www.shunyecasting.com/
